In the bustling world of industrial operations, efficiency and reliability are key to staying competitive. One of the most versatile and widely used pieces of equipment that can greatly enhance productivity is the belt conveyor. Whether you’re handling lightweight items or heavy-duty materials, belt conveyors can streamline your processes, minimise manual labour, and improve overall workflow. In this article, we’ll explore the top benefits of incorporating belt conveyor systems into your industrial facility, with a focus on various types available, including belt conveyors for sale, powered belt conveyor, and more.
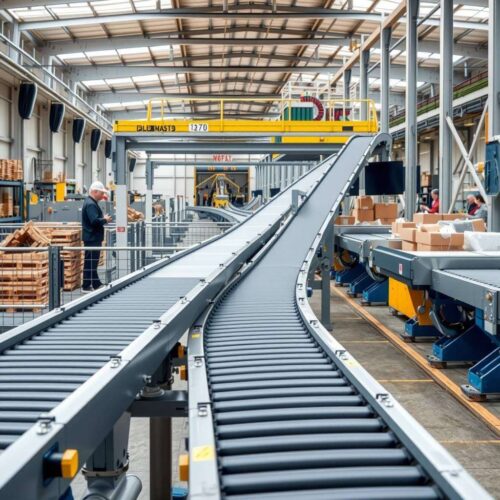
A belt conveyor efficiently transports materials across various industries. Discover an impressive example at https://earthobservatory.nasa.gov/images/150869/worlds-longest-conveyor-belt-system, showcasing the incredible power and design of modern belt conveyor systems used worldwide.
Belt Conveyors for Sale: A Versatile Investment
When considering efficiency upgrades, the availability of belt conveyors for sale offers a great opportunity for businesses of all sizes. These systems are known for their adaptability across multiple sectors—from manufacturing and packaging to logistics and distribution. Buying the right belt conveyor system can be a cost-effective way to optimise operations. Plus, many suppliers offer customised options tailored to your specific needs, including modular belt conveyors and inclined belt conveyors.
Investing in a quality belt conveyor can lead to substantial long-term savings by reducing labour costs and minimising product damage. Many suppliers also provide maintenance and support, ensuring your conveyor operates smoothly for years to come.
Powered Belt Conveyor: Enhancing Automation and Speed
A powered belt conveyor, equipped with a motorised drive system, is a game-changer for automation. These systems are designed to move goods efficiently, with minimal manual intervention. They are perfect for handling high-volume materials or tricky layouts that require consistent speed and control.
The advantages of powered belt conveyors include precise speed regulation, easy integration into automated systems, and the ability to handle heavy or bulky items. Modern powered belt conveyors often come with features like variable speed drives, which allow operators to fine-tune the conveyor’s operation, enhancing flexibility. This makes them ideal for varied manufacturing or distribution needs where product flow and timing are critical.
A belt conveyor is an essential piece of equipment for efficient material handling. For high-quality options, visit https://www.cimbria.com/en/products/conveying/belt-conveyors.html. Belt conveyors are reliable, durable, and suitable for various industries, ensuring smooth transportation of bulk materials while minimizing downtime and maximizing productivity in your operations.
A belt conveyor is an essential component in many industrial and manufacturing processes, allowing smooth and efficient material handling. Its durability and reliability are key for operational success. For high-quality belt conveyors, visit www.conveyorrollers.co.uk for trusted solutions and expert advice.
Belt Conveyor Systems for Sale: Tailoring Your Conveyor Network
Choosing belt conveyor systems for sale provides the opportunity to develop an integrated, customisable conveyor network. These systems can be configured in multiple layouts—linear, curved, inclined, or even vertical—ensuring your facility’s unique layout is optimally utilised.
Belt conveyor systems for sale come in a wide range of specifications and capabilities. From lightweight models suitable for delicate items to heavy-duty belt conveyors designed for tough, industrial environments, there’s an option for every application. Modular belt conveyors, in particular, have gained popularity because of their flexibility: sections can be added, removed or reconfigured as your operational needs evolve. This adaptability helps future-proof your investment and reduces the need for costly replacements.
Belt Conveyors UK: Reliability and Local Support
For businesses operating within the UK, selecting belt conveyors UK suppliers offers advantages in terms of local support, quicker delivery times, and customised solutions suited to the regional industrial landscape. UK-based suppliers often specialise in durable, high-quality systems suitable for heavy industry, warehousing, and manufacturing sectors.
Additionally, they are well-versed in compliance with UK regulations and standards, ensuring your conveyor system meets all safety and environmental requirements. Whether you need a standard conveyor or bespoke solutions, sourcing from UK providers ensures reliable after-sales support and servicing.
Modular Belt Conveyor: Flexibility and Ease of Maintenance
Modular belt conveyors stand out because of their ease of installation, maintenance, and customisation. These belts consist of interlocking modules, usually made from plastics or rubber, that can be easily replaced if damaged. Their design allows for quick assembly and reconfiguration, which is ideal for facilities that undergo frequent changes or need a bespoke setup.
Modular belt conveyors are also excellent for handling various product shapes and sizes due to their smooth, continuous surface. Their flexibility makes them popular in food processing, packaging, and sorting applications, where cleanability and adaptability are essential.
Inclined Belt Conveyor: Moving Items to New Heights
Inclined belt conveyors are invaluable in facilities where products need to be transported to higher levels, such as mezzanines or multi-storey warehouses. They allow for gentle elevation of items while maintaining a steady flow, reducing the risk of product slippage or damage.
Such conveyors are designed with adjustable angles and specialised belts to handle different materials securely. Whether for packaging lines, assembly operations, or storage solutions, inclined belt conveyors optimise space utilisation and help maintain a seamless flow across various production stages.
Belt Conveyor Systems: Streamlining Your Operations
Comprehensive belt conveyor systems are a backbone of modern industrial facilities. They facilitate the movement of goods between different processing stations, storage areas, and packing lines. The key benefits of implementing these systems include increased throughput, consistency in handling, and improved safety by reducing manual lifting and transport.
By integrating various types such as modular, inclined, or heavy duty belt conveyors, companies can create customised systems tailored to specific operational demands. This flexibility helps optimise your facility’s layout and ensures rapid, reliable movement of goods, ultimately increasing overall efficiency.
Heavy Duty Belt Conveyor: Handling Tougher Tasks
For industries dealing with heavy, bulky, or abrasive materials—such as mining, steel manufacturing, or waste processing—a heavy duty belt conveyor is essential. These robust systems are built with durable components engineered to withstand demanding environments and high loads.
Heavy duty belt conveyors can handle materials like stones, scrap metal, or construction debris efficiently and with minimal downtime. Their sturdy frameworks, reinforced belts, and powerful drive systems make them suitable for some of the most rigorous applications, delivering dependable performance over extended periods.
Incorporating belt conveyor systems into your industrial setup offers a host of benefits, from cost savings and efficiency to safety and customisation. Whether you’re browsing belt conveyors for sale or investing in specialised models like modular, inclined, or heavy duty belt conveyors, the key is selecting the right system to match your operational needs. Modern belt conveyor systems are proven allies in driving productivity, reducing manual handling, and creating more streamlined, safe working environments.