In the ever-evolving landscape of industrial operations, belt conveyor technology has remained a cornerstone in the efficient movement of goods. With its origins steeped in the requirements of manufacturing and construction, this technology continues to adapt and innovate, meeting modern demands across various sectors. The latest advancements not only enhance productivity but also embrace sustainability, safety, and flexibility, allowing businesses to thrive in a competitive market.
As the demand for automated solutions expands, many industries are tapping into the benefits that cutting-edge belt conveyor systems offer. From small warehouses to large agricultural facilities, advancements in belt conveyor technology are poised to revolutionise how products are transported, stored, and managed. In this article, we will explore the latest innovations and trends shaping this integral technology.
Belt Conveyors
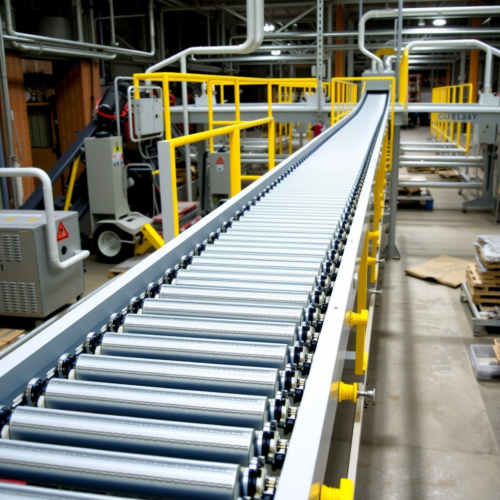
Belt conveyors have long been the backbone of material handling, facilitating the transport of goods over short and long distances within various industrial environments. Recent innovations in belt material and design have significantly improved durability and efficiency. For instance, modular belting has gained traction, offering enhanced adaptability and maintenance benefits. These belts can be easily replaced or configured to meet specific transport needs, minimising downtime.
Moreover, advancements in automation have led to the integration of smart belt conveyor systems equipped with sensors and monitoring capabilities. This innovation allows for real-time data collection, ensuring predictive maintenance and optimised operation, ultimately reducing operational costs and improving overall system reliability.
Belt Conveyor Small
The rise of e-commerce and the need for efficient warehousing solutions have fostered the development of small belt conveyors. These compact systems are designed to fit into tight spaces, making them ideal for warehouses with limited floor space. Innovations such as miniaturised components and modular designs enhance their versatility and ease of installation.
Additionally, small belt conveyors are increasingly incorporating automation features, which allow businesses to streamline their sorting and packaging processes. With the ability to interface seamlessly with existing warehouse management systems, small belt conveyor systems are enhancing all aspects of logistics, from inventory handling to order fulfilment.
Belt Conveyor Manufacturer
With the advancements in technology, the role of belt conveyor manufacturers has evolved significantly. Today, a skilled conveyor manufacturer must not only understand traditional material handling solutions but also stay current with emerging technologies and market demands. Manufacturers are now focusing on producing custom solutions tailored to the specific requirements of their clients.
In addition to customisation, belt conveyor manufacturers are making strides in sustainable practices. Many are investing in eco-friendly materials and energy-efficient designs, catering to a market that increasingly values environmental responsibility. The collaboration between manufacturers and industries is essential in advancing belt conveyor systems to foster a greener future.
Belt Conveyor Systems
Modern belt conveyor systems are more than just simple mechanical transport devices; they are intricate systems designed to optimise the flow of materials. Innovations such as intelligent conveyor software allow for the dynamic adjustment of conveyor speeds based on the volume of products being transported, effectively managing workflow and reducing bottlenecks.
Furthermore, the incorporation of artificial intelligence and machine learning into these systems is groundbreaking. With intelligent algorithms, conveyor systems can predict maintenance needs, evaluate performance metrics, and suggest optimisations, providing manufacturers with invaluable insights to maximise efficiency.
Warehouse Belt Conveyor
In the realm of warehousing, belt conveyors have seen significant upgrades that cater specifically to storage and retrieval processes. Automated warehouse belt conveyors enable a higher degree of precision in inventory management, enhancing how goods are moved through different zones within a warehouse.
Innovations such as high-speed transport systems and integrated sorting features have transformed traditional warehousing operations, allowing for rapid processing of incoming and outgoing goods. These systems have become essential as warehouses adapt to the fast-paced requirements of modern distribution, ensuring that products move swiftly and accurately from storage to shipping.
Agricultural Belt Conveyors
Agricultural operations are also benefiting from advancements in belt conveyor technology, reflecting the sector’s unique challenges in material handling. Agricultural belt conveyors are designed for durability and to withstand harsh environments, enabling the efficient transfer of bulk materials such as grains, seeds, and fertilisers.
Recent innovations include the development of heavy-duty belt conveyors that can transport larger volumes and heavier loads without compromising performance. These systems are equipped with features such as adjustable heights and variable speeds, allowing for greater flexibility in operations. Moreover, manufacturers are integrating monitoring devices that enhance safety and ensure streamlined workflow in agricultural settings.
A belt conveyor is an essential component in various industries, efficiently transporting materials over long distances. Whether in manufacturing or warehousing, these systems enhance productivity and streamline processes. For high-quality options, visit www.conveyorrollers.co.uk, where you’ll find a wide selection of durable belt conveyors tailored to your needs. With the right model, you can optimize your workflow and ensure seamless material handling throughout your operations.
Heavy Duty Belt Conveyor
Heavy-duty belt conveyors are pivotal in industries requiring the transportation of large and heavy materials, such as mining and construction. As demands rise for equipment that can tackle extreme conditions, recent innovations have focused on the strength and resilience of belt materials, leading to longer service life and reduced maintenance costs.
Developments in belt construction technology, such as the use of high-tensile strength fabrics and reinforced designs, have improved load-bearing capacities significantly. Additionally, manufacturers are now incorporating advanced drive technologies that enhance the power and efficiency of heavy-duty belt conveyor systems, optimising energy consumption while sustaining high performance under pressure.
In summary, innovations in belt conveyor technology are redefining the landscape of material handling across various sectors. From small warehouse operations to heavy-duty agricultural environments, the focus on efficiency, customisation, and sustainability is paving the way for future advancements in this essential industry. As we continue to witness these changes, it is crucial to stay informed and adapt to the innovations that can drive success in your operations.