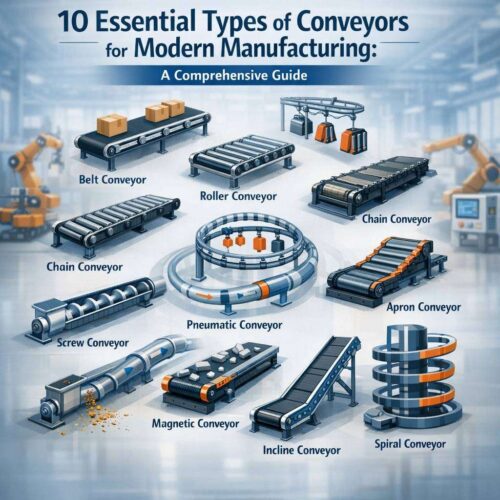
In today’s manufacturing landscape, efficiency, reliability, and adaptability are non-negotiable. Conveyor systems play a central role in streamlining production lines, reducing manual handling, and improving overall workflow. This guide presents ten essential types of conveyors commonly employed in modern factories, outlining their key characteristics, typical applications, and practical considerations. Whether you are upgrading an existing facility or designing a new line, understanding the strengths and limitations of each conveyor type will help you select the most appropriate solution for your operations.
Belt conveyors
Belt conveyors are among the most versatile and widely used conveyor systems in manufacturing. A continuous belt, driven by pulleys, transports goods along a straight or curved route. They accommodate a broad range of products, from small components to palletised loads, and can be configured with different belt materials to suit temperature, humidity, or chemical exposure. Belt conveyors are ideal for high-capacity, long-distance transport and can be belt-modular or belt-driven to suit integration needs with other equipment.
Decline and incline conveyors
Designed to handle elevation change within a line, incline and decline conveyors use belt or roller technology to move goods up or down slopes. They are essential for multi-level facilities or for feeding autonomous systems, such as pick-and-place robots, with gravity-assisted movement or powered assistance. Incline and decline sections can be stationary or part of a powered system with gradient control to manage acceleration and braking, ensuring item integrity and rider safety on steep routes.
Conveyors streamline factory workflows, enhancing efficiency and throughput across production lines. They reduce manual handling and improve consistency, enabling scalable automation. For deeper customization and troubleshooting, consult expert tips and community discussions. https://forum.keenswh.com/threads/how-do-you-research-unlock-conveyor-tubes.7403879/
Roller conveyors
Roller conveyors rely on rotating rollers to convey items, typically with a belt or chain-based drive along the line. They are well-suited to heavy or palletised loads and offer gentle handling for fragile products when combined with variable-speed drives. Roller conveyors provide high durability and are commonly used in buffering zones, assembly lines, and manual-handling stations where throughput may vary.
Gravity conveyors
Gravity conveyors use the natural force of gravity to move goods, usually in a downward or horizontal direction. They are low-cost, low-maintenance options ideal for simple transfer tasks, hand-off points, or storage reclaim zones. Modularity is a strength in gravity conveyors, with components such as skate wheels, roller beds, and line-shaft designs enabling easy reconfiguration.
Powered roller conveyors
Powered roller conveyors combine rollers with a drive mechanism to propel items along the line. They deliver smooth, controlled motion and are effective for irregular-shaped loads or items that require short intervals of movement. These systems can be designed with zone controls, enabling a mix of actively driven and idle zones to optimise energy use while maintaining throughput.
Chain conveyors
Chain conveyors use a chain-driven mechanism to transport goods, often via attached carriers or pallets. They provide robust handling for heavy, bulky, or heat-sensitive items and are common in automotive, metal, and food processing sectors. Chain conveyors offer precise control of motion, strong resistance to wear, and good containment of payloads around curves and inclines.
FAQ: Conveyors
What is a conveyor and how does it work?
A conveyor is a mechanical system that moves materials from one location to another using belts, rollers, chains, or screws. It typically consists of a frame, a drive unit (motor or belt drive), and a powered surface that transports items along a set path. The main purpose is to improve efficiency, reduce manual handling, and streamline production or packaging processes.
What are the different types of conveyors?
- Belt conveyors: use a continuous belt for smooth transport of goods.
- roller conveyors: rely on rotating rollers to move items, often gravity-driven or motorized.
- chain conveyors: use linked chains to carry heavy or bulky loads.
- pallet conveyors: designed to move pallets with a belt or roller surface.
- screw conveyors: use an auger to move bulk materials.
- vertical conveyors: lift or lower items between levels.
- curved conveyors: navigate around corners and obstacles.
- overhead conveyors: suspended systems that move items above the floor.
- magnetic conveyors: use magnets for ferrous materials.
How do I choose the right conveyor for my application?
Consider:
- Type and size of items (shape, weight, fragility)
- Required speed and throughput
- Floor space and layout
- Environment (dust, moisture, temperature)
- Loading/unloading methods
- Maintenance and accessibility
- Total cost of ownership (purchase, installation, energy, maintenance)
What are the advantages of using conveyors?
- Increased throughput and efficiency
- Reduced manual handling and the risk of injury
- Consistent, repeatable movement of goods
- Improved workplace organisation and ergonomics
- Scalable solutions for changing production needs
What maintenance is typical for conveyors?
- Regular inspection of belts, rollers, and drive components
- Tension and alignment checks
- Lubrication of bearings and drive chains
- Cleaning to prevent buildup and corrosion
- Checking sensors, motors, and safety interlocks
- Replacing worn parts promptly to prevent downtime
Are conveyors safe to operate?
Yes, when properly installed and maintained. Safety features include emergency stops, guards, interlocks, photoelectric sensors, and proper training for operators. Always follow manufacturer guidelines and conduct risk assessments.
How long do conveyors last?
Lifespan varies by type, usage, and maintenance. With proper care, many conveyors can operate reliably for 10–20 years or more, though belts, rollers, and motors may require periodic replacement.
Can conveyors be customised for my facility?
Yes. Conveyors can be tailored in length, width, height, incline/decline, speed, and features (diverters, sorters, accumulators, controls). Customisation helps fit unique layouts and process requirements.
What safety certifications or standards apply to conveyors?
Common standards include CE (Europe), UL/CSA (North America), ISO 12100 for safety of machinery, and industry-specific regulations. Always verify compliance for your region and industry with the supplier.
How much do conveyors cost?
Costs vary widely based on type, length, speed, automation, and customisation. Basic gravity conveyors are relatively affordable, while automated, high-throughput systems with sensors and controls can be significantly more expensive. Request a specification-based quote for accurate pricing.
Do conveyors require automation integration?
Many do. They can be stand-alone or integrated into automated material handling systems, including sorters, AS/RS, robotic pickers, and warehouse management systems (WMS). Integration may involve controls programming, sensors, and networking.
What is the installation process like?
Typically involves site survey, design and engineering, procurement of components, installation of frames, belts or rollers, drive and control wiring, safety upgrades, and commissioning. It often requires a collaboration between vendors, integrators, and facility maintenance.
How energy-efficient are conveyors?
Modern conveyors emphasise efficiency with regenerative drives, variable frequency drives (VFDs), energy-efficient motors, and optimised control systems. Properly sized conveyors and smart routing can reduce energy consumption.
Can conveyors handle heavy or fragile items?
Yes, there are conveyors designed for both extremes:
- Heavy items: reinforced frames, steel roller chains, and heavy-duty belts.
- Fragile items: adjustable speeds, cushioning belts, and gentle transfer devices to minimise impact.
What should I consider for maintenance downtime planning?
Plan preventive maintenance during off-peak hours, secure spare parts, train staff on operating procedures, and implement a maintenance calendar aligned with manufacturer recommendations to minimise unexpected downtime.
How do I find a reliable conveyors supplier?
Seek vendors with:
- Industry experience and case studies
- Clear technical specifications and support
- Comprehensive warranty and service options
- On-site assessment or customisation capabilities
- Positive reviews and references
If you’d like, tell me your specific item sizes, throughput needs, and space constraints, and I can help narrow down suitable conveyor types and configurations.
Screw conveyors
Screw conveyors transport bulk materials rather than discrete items. A helical auger within a stationary trough moves material using rotation, making them ideal for powders, grains, granules, and pellets. They provide efficient, sealed handling and are frequently used in dust-tight or sanitary environments where product containment and contamination prevention are critical.
Modular plastic belt conveyors
Modular plastic belt conveyors use interlocking plastic modules to form a continuous belt. They are exceptionally versatile, easy to clean, and resistant to corrosion. The modular design allows for easy repair, quick belt replacement, and simple integration with accumulation zones, lifting devices, or zones of automated inspection. They are well suited to wet or sanitary environments such as food and beverage processing.
Magnetic conveyors
Magnetic conveyors utilise magnetic fields to attract ferrous loads or magnetic carriers along a track. They offer contact-free handling, which can reduce product damage and mark-free transport for delicate or high-value components. Magnetic systems are frequently used where clean, low-friction transfer is essential, such as electronics assembly lines or precision manufacturing environments.
Conveyors streamline workflows by moving materials smoothly from one station to the next, reducing manual handling and boosting productivity. From design and installation to maintenance, modern conveyors are versatile, scalable, and energy-efficient, adapting to diverse industries and spaces. For quality components and trusted guidance, explore https://conveyorrollers.co.uk for durable solutions, service, and support. With the right system in place, teams can improve throughput, safety, and consistency across production lines, while minimizing downtime and operational costs.
Vacuum conveyors
Vacuum conveyors use suction to transport granular, powdery, or small loose items through a sealed conduit. They provide excellent containment and dust control, making them popular in pharmaceutical, food, and chemical industries. Vacuum systems can be configured for closed-loop recycling of materials or integrated with inline sieving and packaging stages.
Considerations for selecting conveyor types
- Throughput and speed: Assess the required rate of movement and the maximum length of line to determine the most efficient drive and control strategy.
- Load characteristics: Weight, shape, size, and fragility influence the choice between belt, roller, chain, or gravity systems.
- Space and layout: Facility geometry, including curves, turns, and elevation changes, guides the layout and type of conveyors that fit best.
- Accumulation and work zones: If lines require buffering, singulation, or automated picking, consider conveyors with built-in zones, sensors, and compatibility with robotics.
- Hygiene and containment: For food, pharmaceutical, or chemical environments, select materials and designs that meet sanitation and containment requirements.
- Maintenance and lifecycle costs: Initial capital expenditure should be weighed against expected maintenance, energy consumption, and parts availability.
Integration and smart features
Modern conveyor systems integrate with factory automation platforms, warehouse management systems (WMS), and manufacturing execution systems (MES). Features such as remote monitoring, predictive maintenance, energy-efficient drive controls, and safety interlocks contribute to superior uptime and safer operations. When designing a system, collaborate with equipment manufacturers to ensure compatibility with control architectures, drive profiles, and safety standards.
Safety and compliance
Safe operation is fundamental. Guarding, emergency stops, overload protection, and clear signage are essential components of any conveyor installation. The use of anti-slip surfaces, properly rated lifting devices, and correct belt tensioning reduces the risk of injury and damage. Compliance with applicable standards and industry regulations should be verified during design and commissioning.
Final thoughts
Selecting the right conveyor types for a modern manufacturing environment involves a thoughtful balance of performance, reliability, and cost. By understanding the strengths and constraints of belt, roller, gravity, chain, screw, modular plastic belt, magnetic, and vacuum conveyors, engineers can craft a cohesive, efficient, and scalable conveyor systems layout. With careful integration and ongoing maintenance, these conveyors will continue to drive productivity, reduce manual handling, and support resilient manufacturing operations.
Discover streamlined material handling with our expert insights into conveyors. From setup to maintenance, our guidance helps you optimize flow, reduce downtime, and boost efficiency across production lines. Explore practical tips, latest trends, and reliable solutions to fit your needs. conveyors empower teams to move products smoothly. Elevate operations and maximize throughput today.