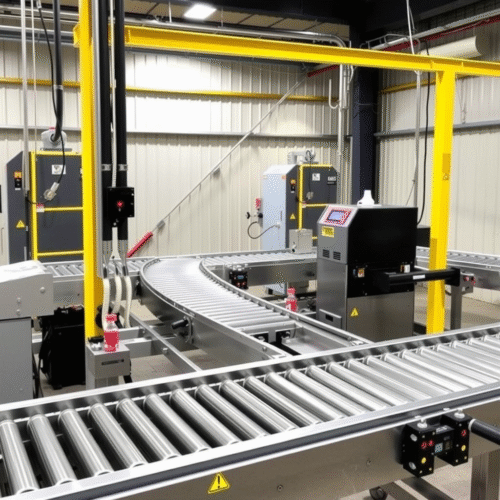
Conveyor systems play a vital role in various industries, enabling the smooth transport of goods and materials. At the core of these systems are conveyor rollers, which are crucial for ensuring efficiency and reliability. As technologies evolve and businesses grow, upgrading conveyor rollers becomes not just beneficial but essential. This article highlights the top five benefits of upgrading your conveyor rollers.
1. Enhanced Efficiency
One of the primary advantages of upgrading conveyor rollers lies in the increased efficiency of material handling. Modern conveyor rollers, such as steel rollers and grooved rollers, are designed to reduce friction and improve the smoothness of the conveyor system’s operation. By switching to high-quality gravity rollers or conveyor belt rollers, businesses can significantly decrease the energy needed for transport, leading to faster processing times and reduced operational costs.
High-performance rollers for conveyors allow for heavier loads to be transported more smoothly, optimising production lines. This is particularly relevant in industries such as manufacturing, warehousing, and distribution, where time and speed are critical to maintaining a competitive edge.
2. Improved Durability
Upgrading your conveyor rollers brings with it the advantage of enhanced durability. Traditional rollers may become prone to wear and tear over time; thus, investing in modern designs, such as sprocket rollers, can mitigate these concerns. The latest materials used in these roller types, including specialised alloys and surface coatings, resist corrosion and abrasion, leading to longer life spans.
For example, UK rollers produced with the specific demands of industry standards can withstand harsh operating environments. This increased resilience means less frequent replacements and maintenance, ultimately driving down the total cost of ownership and minimising downtime due to roller failure.
3. Enhanced Safety
Safety is a paramount concern in any workplace. Upgrading conveyor rollers supports a safer work environment by reducing the risk of accidents related to equipment failure. High-quality rollers, particularly when manufactured precisely to the required specifications, ensure that materials are transported smoothly and securely.
Moreover, using gravity rollers designed for specific load capacities minimises the risk of overload, which can lead to catastrophic breakdowns. Advanced roller designs often come with added safety features, such as rollers with built-in brakes or those designed to prevent misalignment, which further enhances overall safety standards. As businesses prioritise employee safety and compliance with health and safety regulations, upgrading conveyor rollers can be a proactive step in this direction.
A conveyor roller is essential for efficient material handling in various industries. These rollers facilitate the smooth movement of goods, reducing manual labor and increasing productivity. When selecting a conveyor roller, consider factors like load capacity and durability. For a wide range of high-quality conveyor rollers, visit https://conveyorrollers.co.uk to find the perfect solution for your needs.
4. Customisation Options
An often-overlooked advantage of upgrading conveyor rollers is the plethora of customisation options available to meet specific operational needs. Today’s manufacturers offer a range of roller types, including adjustable-height rollers, different diameters, and varied material compositions, ensuring that businesses can find the most suitable upgrade.
For instance, a company working with heavier loads may benefit from larger steel rollers, whereas a facility needing flexibility in handling diverse product types might prefer grooved rollers that accommodate various shapes and sizes. This customisation can optimise the operational flow, allowing businesses to tailor their conveyor systems to meet specific production requirements, simplifying material handling, and enhancing productivity.
5. Reduced Noise and Vibration
Another significant benefit of upgrading conveyor rollers is the reduction of noise and vibration during operation. Older rollers may generate excessive noise due to wear or improper alignment, which can contribute to an uncomfortable work environment. In contrast, modern rollers, particularly those utilising advanced bearing technologies, operate more smoothly and quietly.
Minimising noise levels enhances occupational comfort and allows personnel to focus better on their tasks. Furthermore, reducing vibration can lead to less wear on other components of the conveyor system, resulting in further maintenance savings and extending the life of the conveyor itself.
Summary
In summary, upgrading your conveyor rollers is vital for enhancing efficiency, improving durability, ensuring safety, providing customisation options, and reducing noise and vibration in the workplace. As industries continue to evolve, so must the technology that supports them. Investing in modern conveyor roller solutions is not only pragmatic but also a strategic decision that can lead to significant operational improvements.
As you explore the possibilities for upgrading your conveyor rollers, consider your specific operational demands and challenges. With the right upgrades, you can ensure that your conveyor systems remain effective and efficient, driving your business towards continued success in a competitive landscape.